On this page
A soluble powder is judged entirely after the event. In the bag it is a white powder that looks the same whether it will dissolve in seconds or leave a lump on the tank floor. Nothing on the outside tells you which — and unlike a liquid, you cannot see stratification or sediment before you commit.
1. What "SP" commits you to
SP stands for soluble powder. The defining requirement is not that it is a powder, but what happens after it meets water: the formulation must be applicable as a true solution of the active ingredient. Not a suspension, not a dispersion — a solution.
That is a stronger commitment than it sounds. It means every particle of active must end up dissolved, and anything that does not dissolve is either an intentionally insoluble inert or a defect. The practical consequences follow from there:
- No agitation to keep it uniform. Once dissolved, it stays dissolved — there is no emulsion to break and no suspension to settle.
- No solvent. Which is why SP is the form of choice where solvent handling, odour or transport classification are constraints.
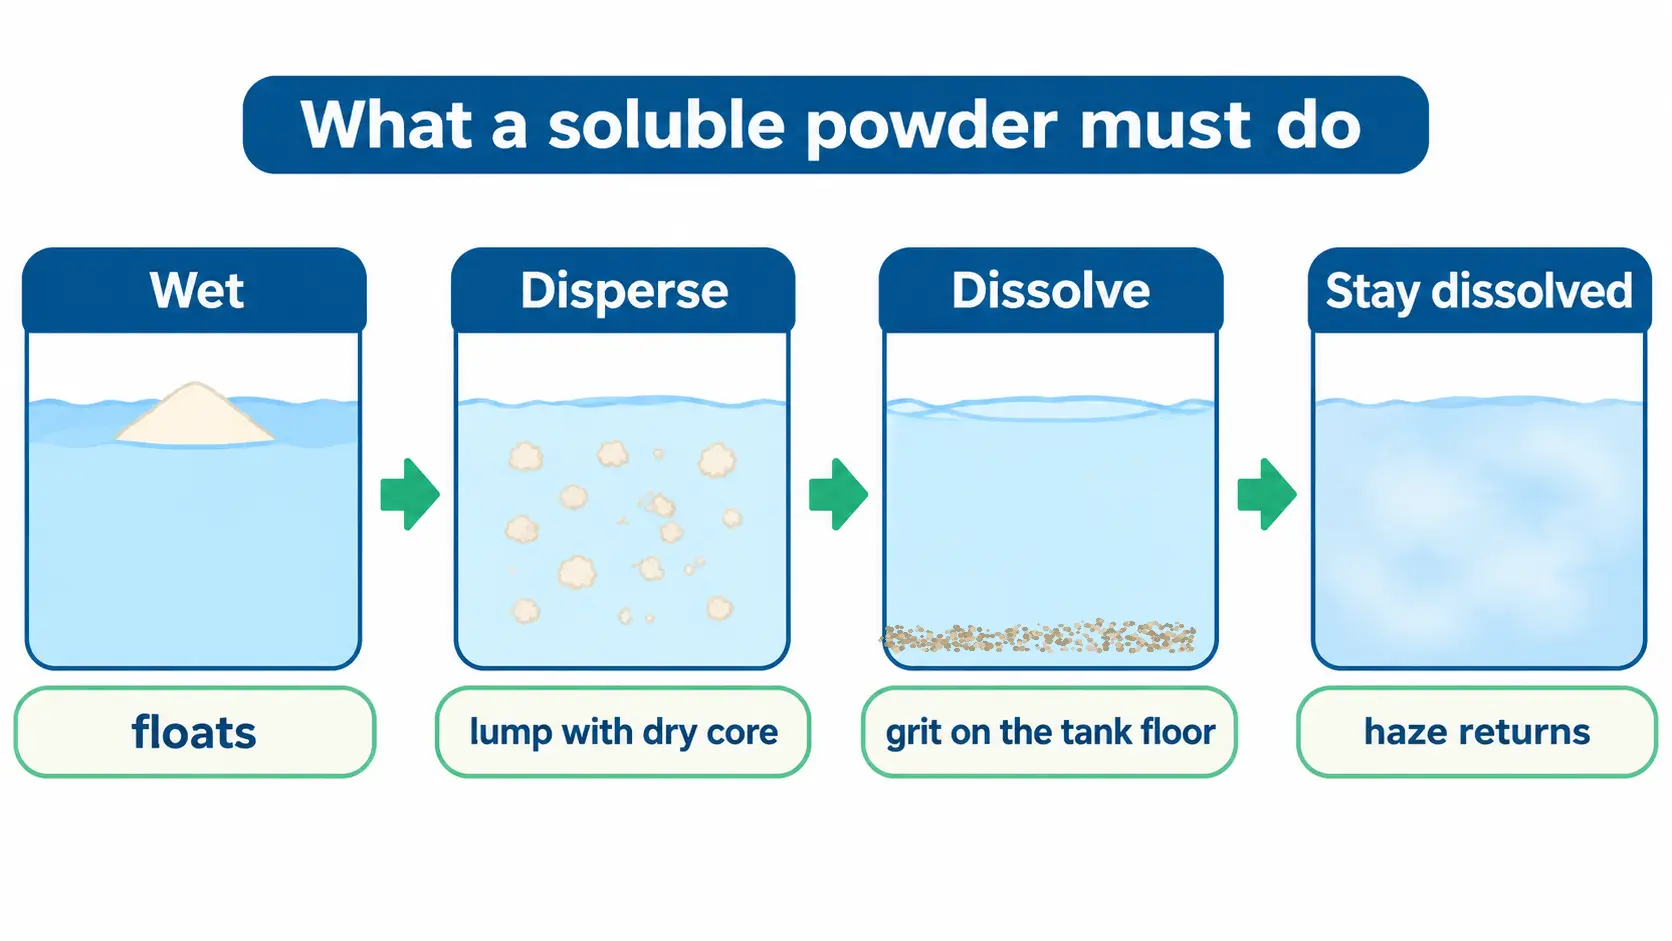
- But the whole burden moves onto dissolution. A liquid that is wrong shows up as haze or separation. A powder that is wrong shows up as undissolved grit, blocked filters, or a tank that never clears.
Our 85% SP is supplied as a water-soluble powder in sachets from 100 g to 1 kg, in 25 kg kraft bags with a PE liner, and in 25 kg fibre drums. 2,4-D sodium salt 85% SP.
2. Wetting and dissolving are two different things
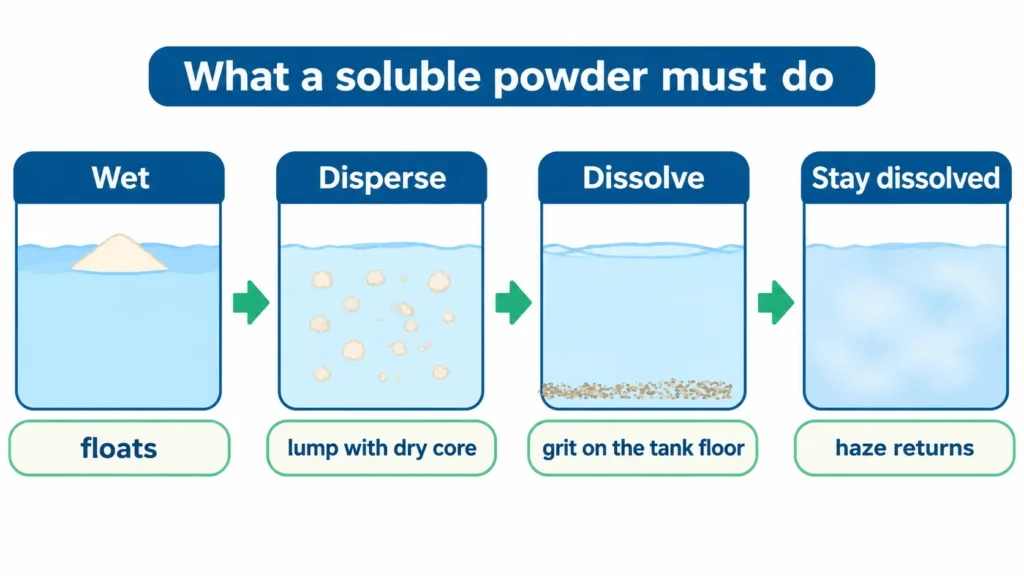
A powder that wets instantly can still form a lump with a dry core. Water reaches the outside, the surface hydrates and gels, and the gel layer slows further penetration. The lump floats, looks wetted, and never dissolves. Operators often read this as “it dissolved, there’s just some foam”.
Why a supplier’s wetting figure tells you very little on its own
A fast wetting time is easy to achieve and easy to quote. It says the powder accepts water quickly. It says nothing about whether the active actually goes into solution, or whether the solution stays clear once it has.
That second half — solution stability — is the one that matters commercially, because it covers what happens between mixing and spraying. A tank that is clear when mixed and hazy after standing is a tank that will block something.
3. The sieve residue test, and what it catches
The dissolution test ends with a physical check: the diluted sample is passed through a 75 µm test sieve, and what stays on the sieve is weighed. That residue is the part that did not dissolve.
The reason the test exists is specific. As the FAO specification guidance puts it, this check detects coarse particles — arising from impurities in the technical material or present as inert ingredients — which could block nozzles and filters in the application equipment.
The failure point is not the tank, it is the nozzle. A hundred grams of undissolved material spread across a hectare is invisible in the field; the same material concentrated in a nozzle is a stopped spray. This is why the test is a specification clause and not a formality.
The test is run in standardised water and read twice — shortly after mixing, and again after standing. The second reading is what separates a powder that dissolves from one that merely dissolves for now.
Two sources of coarse particles
Worth knowing where the problem comes from, because it changes who owns it:
- From the technical material — coarse or poorly milled active, or impurities that do not dissolve
- From the inert ingredients — a filler or carrier chosen for cost rather than solubility
A buyer negotiating on price alone is effectively negotiating over the second one. The cheapest filler is usually the one that leaves the most on the sieve.
4. Dust, flow and the person holding the scoop
Most of the discussion about powders concerns the machine. There is a human at the other end of the bag, and a powder behaves differently in a scoop than in a tank.
Flow
Free-flowing powder pours; a powder that has begun to cake does not. This matters at the weighing step: an operator dosing by volume gets a different mass depending on how the powder flows that morning, and a dose that is right on a dry day can be wrong after a humid week.
Dust
Fine particles become airborne when a bag is opened and poured. That is an operator-exposure issue first and a housekeeping issue second — dust settles on surfaces, migrates on air movement, and is difficult to clean out of a warehouse once it is there.
A dusty powder is a handling cost that transfers with the goods. If your customer’s operators need respiratory protection and a cleanup routine just to open a 25 kg bag, that is friction on every order — and it is the kind of friction that gets a supplier replaced quietly, without complaint.
What this means for packaging
It is one reason soluble powders are often supplied in water-soluble sachets at the smaller end: the sachet goes into the tank whole, so the powder is never poured and never becomes airborne. Above that size, a lined bag with a clean pour lip does most of the work. Packaging options for sachet, lined bag and fibre drum.
5. Moisture, caking and storage
Every problem in this article gets worse with moisture, and moisture is the one variable a buyer controls least — it depends on the warehouse, the season, and how long the bag sat before it was opened.
What moisture does
- Caking. Particles bridge into lumps under the weight of a stacked pallet. Once a bag has caked, the powder no longer flows and dosing becomes guesswork.
- Slower dissolution. A partially hydrated particle has already begun to gel at its surface, which is exactly the barrier that stops it dissolving fully later.
- Assay drift on paper. A product declared on a dry basis will read low if it has taken up water — the active has not changed, the denominator has.
What actually protects it
The inner liner
Stack height and pallet practice
Floor contact and airflow
Stock rotation
6. What to check on arrival
Four checks, in this order, all of them cheap.
For the liquid forms, the same principles take different shapes: dilution water and hard-water behaviour in 2,4-D DMA salt 720 g/L SL: handling and compatibility, and emulsion behaviour in 2,4-D isooctyl ester EC: reading emulsion stability. For the raw material behind all of them, 2,4-D 98% technical material covers assay and impurity profile. To compare the forms on acid equivalent before choosing, see the 2,4-D form comparison.
Send us the water your customer will dissolve in and the pack format you need. We will confirm the dissolution behaviour and quote with the batch documentation, within one business day. Send us your water and pack format.
Sources
Formulation requirements and test methods are taken from the FAO/WHO specification guidance for water soluble powders.
FAO / WHO — Manual on the Development and Use of FAO and WHO Specifications for Pesticides, section 6.21 Water Soluble Powders (SP)